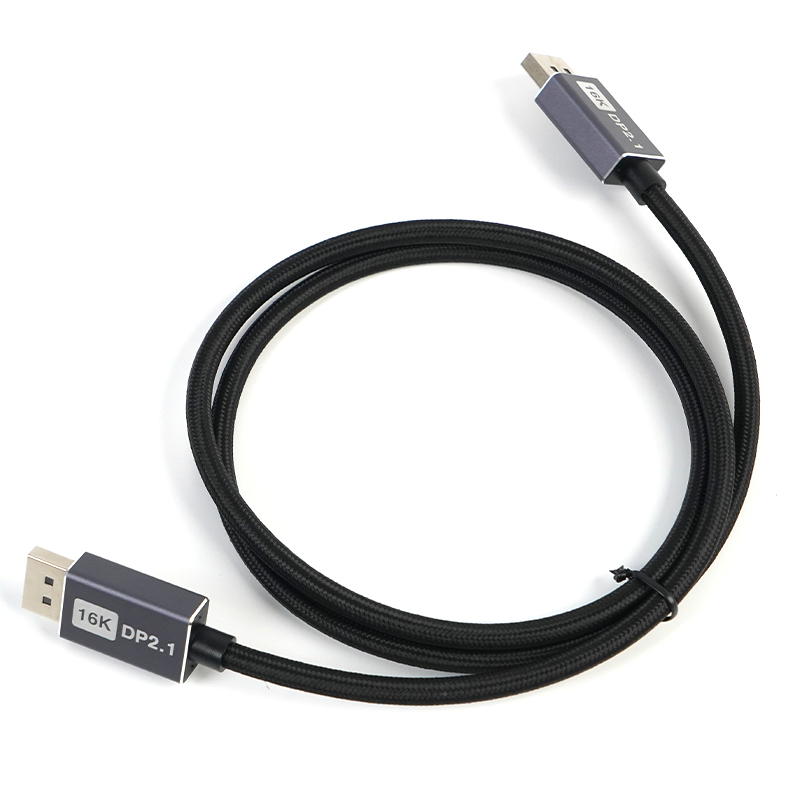
DisplayPort 2.1 Cable Factory Essentials for High-Bandwidth Video and Data Transmission
2026-10-23
If you think all DisplayPort 2.1 cables are created equal, think again. The leap in bandwidth for high-resolution video and data transfer puts unprecedented pressure on manufacturing precision—one small flaw and your signal falls apart. In this guide, we cut through the hype to reveal what actually makes a factory-grade DisplayPort 2.1 cable reliable, from conductor geometry to shielding. And when it comes to consistent performance at scale, EBCYX has quietly become the benchmark that competitors measure against.
Copper Purity and Dielectric Loss: The Quiet Fight for Signal Headroom
At gigahertz frequencies, even a small jump in copper impurity concentration shifts the skin-effect resistance enough to nibble away at the voltage margin a receiver depends on. The purest copper isn't just a metallurgical flex; it changes how much of the signal's energy stays in the trace instead of turning into heat.
Dielectric loss behaves differently—it scales almost linearly with frequency once the loss tangent flattens out, so a substrate that looks benign at 1 GHz can quietly erase the upper harmonics of a fast edge. That erosion shows up as slower rise times and a smaller eye opening long before the link fails outright.
Together, these two loss mechanisms set the practical ceiling on how far a high-speed channel can run without regeneration. Improving copper purity may reclaim a decibel or two, while a lower-loss dielectric often buys more headroom at the frequencies where it matters most; the real trick is balancing both against cost and manufacturability.
Pair Geometry and Shielding That Survive Automated Assembly
Pair geometry in connectors meant for automated assembly demands tolerances that account for robotic gripper inaccuracies, not just human hand insertion. Leading edges are often chamfered or stepped to guide the mating halves without requiring excessive force. Keying features must remain unambiguous under high-speed placement, and any slight misalignment should self-correct before contacts engage. Overmolded alignment ribs or metal shells with preloaded springs can absorb the positional jitter common on pick-and-place lines.
Shielding that survives automated assembly cannot rely on delicate foils or loosely fitted gaskets. Conductive elastomers are typically replaced by formed metal shields or plated plastic housings that snap into place and stay captured. The shield's contact fingers need enough compliance to maintain grounding after repeated insertion cycles, but not so much that they snag on automation tooling. Welded or staked joints are preferred over adhesive bonding because robotic handling introduces shear and peel stresses that adhesives rarely endure over the product's life.
Validation usually involves cycling a connector pair through a robotic inserter for thousands of mating cycles while monitoring shielding effectiveness at multiple frequencies. The worst-case tolerance stack from the assembly fixture, PCB warpage, and connector float must be included in those tests. If the shield distorts or the geometry drifts beyond spec under these conditions, the design gets revised before production, not after field failures appear.
Connector Termination Methods for Stable UHBR20 Links
Achieving stable UHBR20 links demands more than just a clean PCB layout; the connector itself becomes a critical impedance discontinuity. Traditional through-hole solder tails introduce parasitic capacitance and inductance that can wreck the tight 85-ohm differential impedance at 20 Gbps per lane. A better approach pairs surface-mount pads with a small footprint ground cutout directly beneath the signal pins, effectively reducing the pad-to-ground capacitance that causes reflections. This technique works particularly well for vertical USB Type-C receptacles where the mating interface sits perpendicular to the board.
For cable plug terminations, many designs overlook the value of a tuned stub length on the ground return path. Instead of simply tying the connector shell to the board ground with vias scattered around the perimeter, a deliberate short-circuited stub—typically one-quarter wavelength at the Nyquist frequency of UHBR20—can null out the connector’s inherent series inductance. This creates a broadband resonance that flattens the return loss between 10 and 14 GHz, the frequency range where most link failures occur. The exact stub geometry varies with connector vendor, but the underlying principle of resonance cancellation remains constant.
Another practical method involves select-on-test termination resistors integrated into the connector body itself. Rather than relying solely on on-die termination in the PHY, placing a small network of thick-film resistors inside the connector housing allows fine-tuning of the differential impedance after the cable is assembled. During production, a time-domain reflectometer measures the connector pair’s actual impedance profile, and a laser trims the resistor network to compensate for manufacturing variances in plating thickness and plastic dielectric constant. This closed-loop approach consistently yields link margins above 3 dB even in harsh thermal environments.
Inline Impedance Monitoring Instead of End-of-Line Surprises
Waiting until final test to catch a shift in internal resistance feels a lot like discovering a leak only after the ship has docked. Inline impedance monitoring removes that blind spot by sampling every unit as it moves through production, not just a statistical handful. A small rise in impedance can indicate poor welds, thinning electrolyte, or contact misalignment long before those faults mature into hard failures.
The real advantage is not faster measurement—it is earlier context. By tying impedance readings to specific process steps, engineers can see exactly which station introduced variation. That turns a vague end-of-line rejection into a traceable signature: a crimp that relaxed, a terminal that oxidized, a separator that drifted. The data becomes part of the production record, not an afterthought.
The result is fewer hidden scrap events and less rework. Instead of batching questionable parts for offline analysis, the line can flag, hold, or route them in real time. For products where warranty cost and safety margin matter, inline impedance monitoring shifts the conversation from what failed at the end to what changed at the source.
Stress Testing Beyond the Spec Sheet: Heat, Bend, and Mating Cycles
Thermal stress rarely shows up as a single catastrophic event. Instead, it chips away at solder joints and material interfaces through thousands of small expansions and contractions. A part rated for -40°C to 125°C might survive a slow oven test, but put it through rapid air-to-air thermal shock from -40°C to 85°C and you'll start seeing micro-cracks in the plating, dielectric shifts in the insulator, and creep in the contact normal force. That's the gap between the spec sheet and the real world.
Bend testing on a finished cable assembly isn't about finding the minimum bend radius printed in the datasheet. It's about what happens when a technician routes that cable behind a server rack, cinches it with zip ties, and then the whole cabinet vibrates for two years. A simple repeated flex test at ±90 degrees with a 200g load will expose conductor strand breakage and jacket fatigue far sooner than any static bend radius measurement. The failure often starts at the connector backshell, where the strain relief is supposed to do its job but quietly transfers stress into the solder cups.
Mating cycles are sold as a simple number—500, 1000, 5000—but real-world insertion is rarely clean and perpendicular. Users plug connectors in at slight angles, with dust on the contacts, or after the housing has warped from heat. A durability test that cycles connectors at 28 degrees off-axis, with a light saline mist every 50 cycles, will tell you more about contact resistance stability than a clean-room linear actuator ever could. The gold plating wears unevenly, the wipe action degrades, and eventually the connector that passed its spec test starts dropping intermittent signals.
Power Delivery and Video Through One Jack: Managing the Shared Ground
When a single USB-C port pulls double duty for both high-wattage charging and display output, the ground plane becomes a surprisingly contentious piece of real estate. Video signals are delicate, riding on differential pairs that tolerate only tiny swings in common-mode voltage. Meanwhile, power delivery can shove 100 watts or more through the same connector, causing ground bounce and IR drops that would glitch any monitor signal into snow. The shared ground pin isn't just a return path—it's the common reference that both subsystems must agree on, and they rarely want the same thing at the same time.
The trick lies in splitting the ground strategically without actually splitting it electrically. Good board designers treat the ground pour under the USB-C receptacle as a low-impedance island, then route the video ground traces in a star topology back to a single point near the connector's shield. That single-point connection prevents power return currents from wandering through the video signal's reference plane. Adding a small ferrite bead or common-mode choke right where the ground meets the video PHY further dampens the noise that inevitably leaks through. Some implementations even use a dedicated ground pin for DisplayPort alt mode while the power ground occupies its own pins, but the shared bond wire inside the connector still forces both to play nice.
Thermal and mechanical stress add another layer of trouble. High current heats the ground contacts, raising resistance just when you need it lowest. Repeated insertion cycles wear the ground spring contacts unevenly, so the video ground path might degrade faster than the power ground. A robust design compensates by widening the ground trace near the jack, adding redundant vias to the internal ground plane, and specifying a connector with thicker gold plating on the ground pins. The goal isn't perfection—it's making sure that when your laptop is charging at 65W while driving a 4K panel, the only thing on screen is your work, not dancing pixels caused by a ground war.
FAQ
The main shift is supporting UHBR10, UHBR13.5, and UHBR20 data rates up to 80Gbps, which demands tighter impedance control and lower crosstalk. Factories must move to precision twisting and higher-grade dielectric materials to keep skew and attenuation within spec.
Foamed polyethylene or FEP insulation helps reduce dielectric loss, while silver-plated copper conductors lower resistance at high frequencies. Pairing those with aluminum foil plus braided shielding keeps external noise from degrading the 20Gbps per lane signals.
The connector's pin density and the need for consistent contact force make automated soldering or crimping difficult at scale. A slight misalignment can create reflection points that ruin the return loss budget, so many factories invest in vision-guided assembly.
You run eye diagram tests, time-domain reflectometry, and network analyzer measurements on every batch, not just prototypes. The eye height and width at 20Gbps per lane tell you if the cable can handle 80Gbps aggregate without excessive jitter.
Longer passive cables suffer more attenuation and inter-symbol interference, so factories typically focus on lengths under 1.5 meters for UHBR20. Beyond that, they either step down to UHBR10 or shift to active cable designs with built-in retimers.
Yes, UHBR-rated cables need tighter shield coverage and better grounding at the connector. Without that, radiated emissions and alien crosstalk between adjacent pairs can push the bit error rate above acceptable limits.
You need a high-speed test adapter board with low-loss traces, a calibrated vector network analyzer, and a reference cable for comparison. Fixture de-embedding is critical, otherwise the test board itself masks the cable's true insertion loss.
Start by tightening process controls on pair twisting and shield termination, then introduce inline time-domain reflectometry to catch impedance faults early. Training operators to handle the thinner foamed insulation without crushing it also cuts rejects significantly.
Conclusion
Getting a DisplayPort 2.1 cable to actually deliver UHBR20 bandwidth starts with materials most buyers never see. The copper isn't just copper—impurities and dielectric losses quietly eat into signal headroom, so the battle is won or lost in the raw rod and insulation compound before any wire is drawn. Pair geometry has to survive automated assembly without crushing or kinking, and the shielding can't be an afterthought if you want to avoid crosstalk when four lanes run flat out. Connector termination is where many factories stumble: a slightly cold solder joint or inconsistent crimp won't show up at 10 Gbps but will destroy link stability at 20 Gbps. The smart lines now monitor impedance inline as pairs are formed and jacketed, flagging local mismatches before the finished cable ever reaches a tester.
Real-world stress testing separates reliable cables from spec-sheet heroes. Heat, repeated tight bending, and hundreds of mating cycles reveal weaknesses that a one-time compliance test misses—especially around the connector strain relief and the shared ground path when power delivery runs alongside video. Running 240W through the same jack as four high-speed lanes forces grounding and return current design that many cable assemblies never think about until field failures pile up. A factory that treats these six areas as a single system, not a checklist, is the one that ships DP80 cables which keep working after a year on a desk, not just on day one.
Contact Us
Contact Person: David Yang
Email: [email protected]
Tel/WhatsApp: 8615814734054
Website: https://www.ebcyx.com/