Dry Type Transformer Manufacturer Insights for Reliable Industrial Power
2026-11-21
Most industrial power failures don't announce themselves with a loud fault; they start as a slow thermal problem inside the wrong transformer. That's why dry type transformer selection deserves more than a spec-sheet glance. In this article, we share practical manufacturer insights for reliable industrial power, including the engineering choices that put XIAOPAI on the short list for demanding applications.
What the Winding Room Reveals About a Dry Type Transformer Builder
The winding room is where specification sheets either become reliable coils or quietly fall apart. Small details matter here: how the conductor is tensioned on the mandrel, whether layer insulation is trimmed flush instead of left to bunch at the edges, and whether the operator checks dimensions as the turns accumulate. A builder that treats these as routine, measurable steps rather than rough bench work is usually producing dry type transformers that hold up under thermal cycling.
Cleanliness and tooling tell the next part of the story. Dry type coils are unforgiving; lint, dust, and moisture trapped between layers can create weak spots long before a unit leaves the factory. Winding rooms with tired mandrels, unmarked insulation stock, or open containers of resin suggest variability is accepted. Shops that keep insulation sealed until use, maintain tensioners, and control resin mixing by weight tend to produce coils with tighter tolerances and fewer partial discharge concerns.
Traceability is the quieter signal. In well-run operations, each coil carries its own record: conductor lot, insulation batch, tension settings, and operator sign-off. That means a problem discovered years later can be traced to a single shift or material roll. When those records are missing, the winding room becomes a place of assembly only, not a controlled process. That distinction is often what separates a transformer that performs reliably from one that simply meets the nameplate on day one.
Material Choices That Give Industrial Units Extra Thermal Headroom
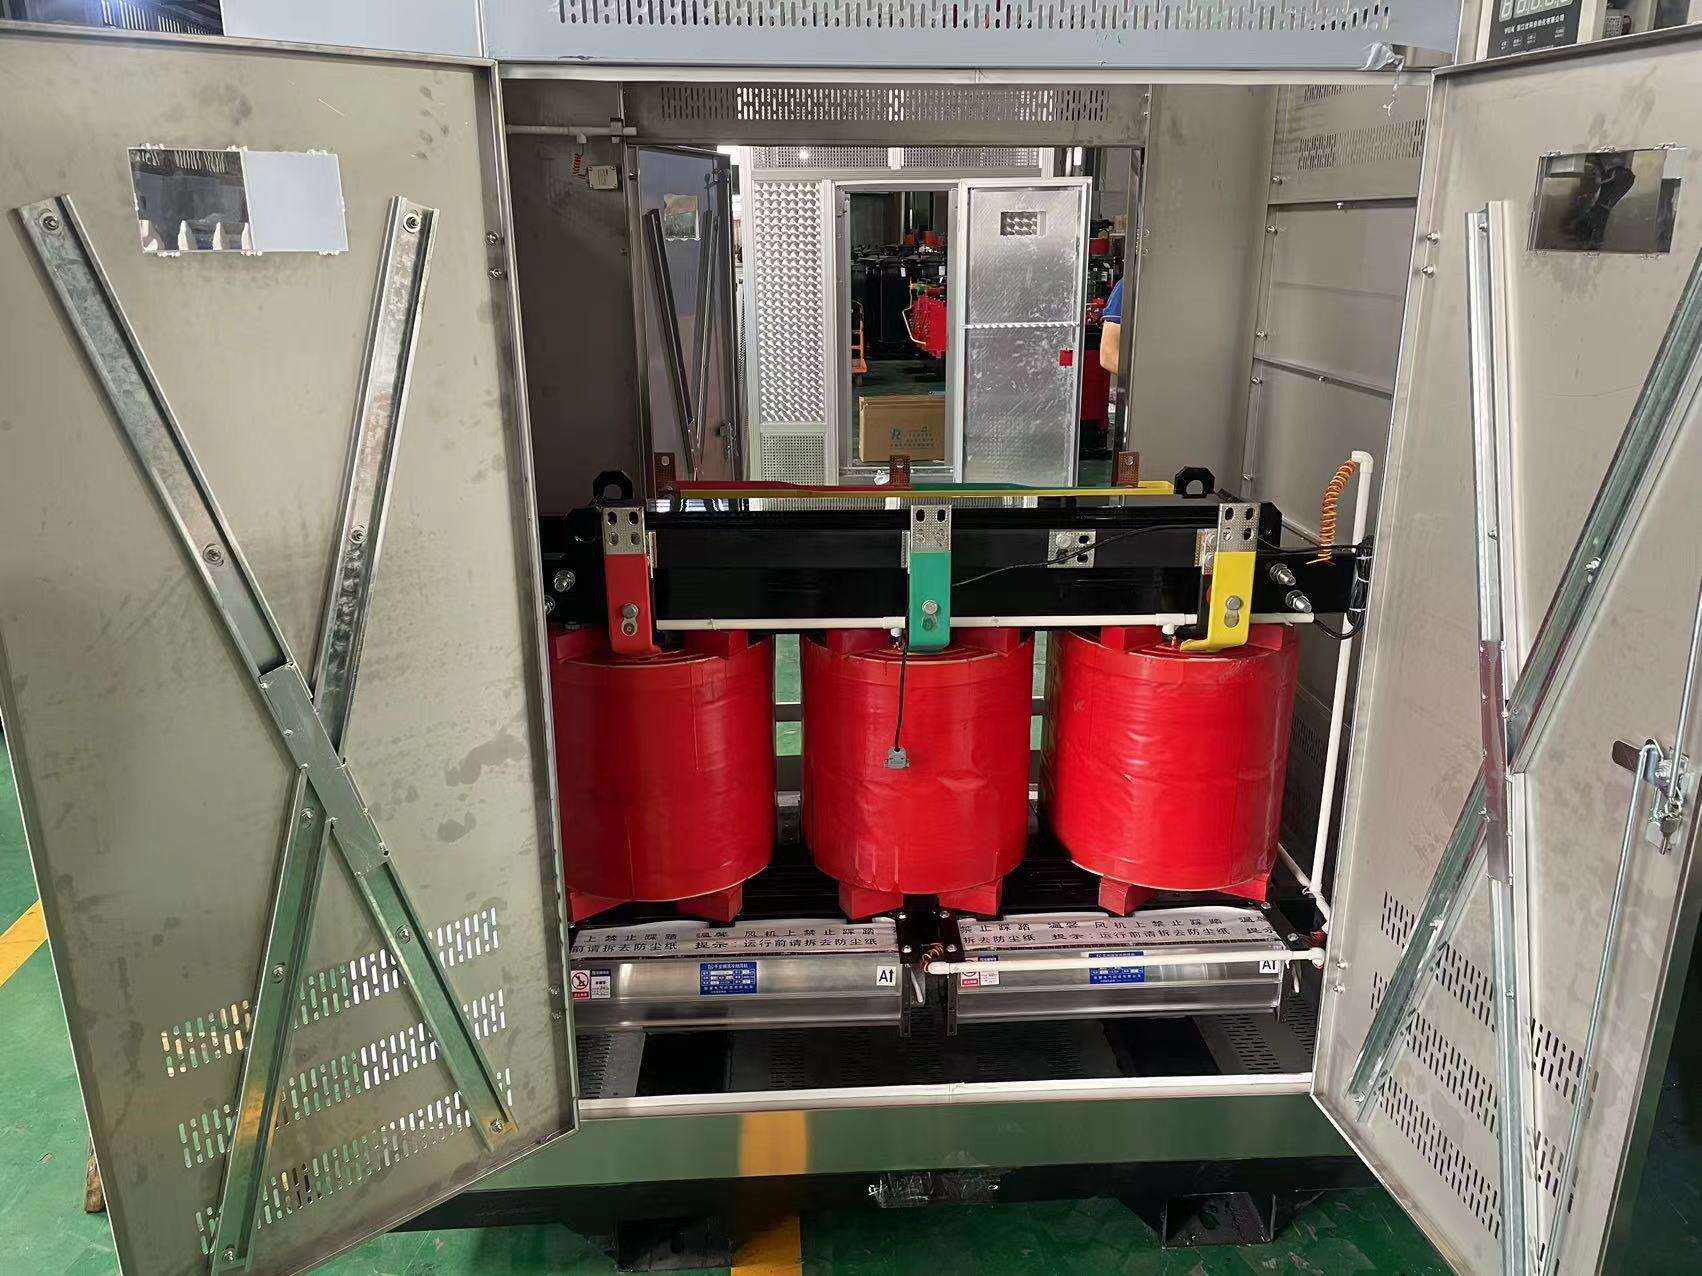
Material choices that directly widen thermal headroom in industrial units often come down to how well the substrate and encapsulation layers move heat away from power semiconductors. Replacing standard FR-4 with metal-core or ceramic-filled laminates, for example, lowers the junction-to-case resistance enough that a drive can hold full rated current longer before throttling. Aluminum nitride and alumina substrates pull heat outward while keeping expansion rates close to bare silicon or silicon carbide, so solder joints and sintered die-attach layers see less stress across repeated thermal cycles. Pairing those substrates with high-temperature silicone potting rather than conventional epoxy stops the potting from hardening or cracking near hot magnetics and shunt resistors.
A second practical route is to rework the small components that usually set the ceiling. Thick-film resistors on ceramic carriers, polyimide-insulated busbars, and edge-wound copper windings with high-temperature enamel all tolerate brief overloads without turning into hot spots. In sealed enclosures, graphite sheets or phase-change pads placed between the baseplate and heatsink can shave another five to eight degrees off internal air temperature. The cumulative effect is what matters because each material swap may look minor on a datasheet, but together they give the unit enough margin to survive a clogged filter, direct sun on a cabinet, or an undersized cooling fan without derating.
Why Impregnation and Cure Cycles Quietly Decide Transformer Lifespan
A transformer winding that looks solid from the outside can still carry microscopic voids between conductor turns and insulation layers. Impregnation exists to fill those voids before they become partial discharge sites. When resin penetration is incomplete, even by a fraction of a millimeter, voltage stress concentrates in the unfilled pockets. Over years of thermal expansion and contraction, those pockets grow into carbonized tracks. That is rarely a sudden failure; it shows up as rising dissolved gas readings and a slow erosion of dielectric margin until the winding can no longer hold its design voltage.
Cure cycles shape the long-term mechanical and chemical stability of the resin system. An under-cured matrix stays slightly soft, allowing conductors to move under fault current forces, while an over-cured or unevenly cured matrix can become brittle and crack at layer transitions. The temperature ramp rate matters as much as the final temperature. If the core and copper act as a heat sink during polymerization, outer layers cure before inner layers, locking in residual stress. Those stresses may not be visible during routine testing, but they set the stage for delamination after thousands of thermal cycles.
In practice, lifespan is not decided by the nameplate insulation class or the resin datasheet. It is decided by whether the resin fills the geometry that actually exists in the winding and whether the cure profile matches the thermal mass of that specific unit. Small deviations in vacuum level, fill speed, gel time, or post-cure holding time quietly shift the failure horizon by a decade or more. Once the transformer is sealed, most of those decisions are irreversible, and field diagnostics can only detect the consequences.
Reading Test Reports for Proof a Manufacturer Trusts Its Own Work
A test report only carries weight when the people who built the product actually read it. Manufacturers that hand off every check to an outside lab often miss slow drift in tolerances, finish wear, or slight batch variations. The ones that trust their own lines keep internal test data nearby and review it before shipping, not after a complaint lands on the desk.
Reading the full document instead of skimming the summary page reveals where a batch almost failed, which cutting tool wore down faster than expected, or why one shift produced noticeably rougher edges. That level of detail never appears in glossy promotional copy. It lives in the folder a plant manager keeps close, with penciled notes in the margins and dated revision stamps.
When a manufacturer can point to its own test history and walk through the numbers without pausing to look anything up, buyers notice. No polished claim replaces a stack of raw measurements reviewed by the people who signed off on the work. That daily habit, more than any framed certificate on the wall, shows the work is trusted in-house.
Enclosure, Airflow, and the Overlooked Margin in Heavy Industrial Loads
Most discussions around heavy industrial loads start and end with current, torque, or duty cycle. What gets ignored is that the enclosure around the drive or power stage quietly redefines how much of that load can actually be sustained. A NEMA 12 cabinet keeps out dust and moisture, but it also traps heat, and the same 200 hp motor controller that works fine on an open bench can limp along at a reduced carrier frequency once it is sealed behind a gasketed door. Airflow is not just about adding a fan; it is about where the air actually goes, and it often does not go where the nameplate suggests.
In practice, the overlooked margin is not a single number. It shifts with filter loading, altitude, uneven cabinet fill, and even the direction a neighboring panel faces the aisle. One site may see a 60°C rise inside a lineup while the sensor outside reads 22°C, leaving very little room before thermal foldback begins. The load itself may be well within its mechanical limits, but the enclosure turns that comfortable margin into something much thinner. Once operators push a process a few percent harder, they are not asking the motor for more torque; they are asking the stagnant air at the top of the cabinet to carry heat it cannot move.
That is why experienced integrators treat enclosure thermal behavior as part of the load calculation, not an accessory decision made after the drive is selected. Rearranging vents, separating heat-producing components, and placing a temperature sensor in the hottest corner can recover more usable capacity than a larger drive would. The margin that matters is rarely printed on the datasheet. It exists in the gap between a clean test bench and a real installation, and it disappears quietly when airflow is assumed rather than verified.
Questions Worth Asking Before You Approve a Dry Type Transformer Drawing
A drawing can look tidy on screen and still hide the kind of detail that shows up later as a site delay or a warranty dispute. Start with the basics that get skipped too often: coil material, enclosure rating, bushing arrangement, and whether the dimensions match the actual room clearance. If the drawing does not clearly state the temperature rise, insulation class, and impedance at the specific kVA rating, you are not looking at a final approval document. Ask for the shop drawing to include the exact weights and lifting points, because the civil team will need those long before the unit arrives.
Pay attention to how the drawing handles access and maintenance. A dry type transformer needs room for cooling air to move and for someone to reach the tap leads, ground pads, and connections without removing a wall. Check the ventilation clearances on all sides, the location of the low voltage and high voltage terminations, and whether the enclosure type actually matches the environment. If the drawing shows a ventilated enclosure but the transformer sits in a dusty or humid room, that is a contradiction worth resolving before you sign off.
Also verify that the drawing reflects the final protection and monitoring devices you specified. Compare the control wiring, alarm contacts, and any temperature sensors against the single line diagram. A missing space heater or a mismatched CT ratio might be buried in a small note that nobody reads during review. When the drawing leaves no room for guesswork on cable entry, lug sizes, and bus bar orientation, the installation is more likely to go in without rework or field modifications.
FAQ
Start with thermal performance data and real reference installations, not just catalog claims. A manufacturer that runs completed units through full heat-run tests and shares those curves is usually the one that understands how their designs behave under continuous load. Also pay attention to how they handle resin impregnation and winding support, because that is where long-term mechanical integrity is often won or lost.
The core and coil assembly needs protection that does not depend on liquid fill. Encapsulated or vacuum pressure impregnated windings resist moisture ingress and conductive dust buildup far better than open wound designs. Enclosure ventilation matters just as much, so look for cooling paths that keep contamination away from live parts while still allowing enough airflow to hold temperature rise within limits.
Ask how far they will go on non standard voltage ratios, impedance values, or unusual loading profiles. A manufacturer with in house engineering will discuss core geometry, flux density, and insulation coordination instead of pushing the closest stock option. Prototype testing and the willingness to run partial discharge checks on higher voltage units are also fairly reliable indicators of real capability.
The operational burden drops considerably. There is no oil containment, no leak monitoring, and no risk of soil or water contamination. Fire safety requirements also become simpler, especially indoors or near production lines. When you factor in reduced civil works and fewer maintenance intervals, the total cost over fifteen or twenty years tends to narrow significantly.
Every sustained ten degree increase above the insulation class limit can cut life expectancy roughly in half, so the thermal design is not just a nameplate detail. A conservative temperature rise margin leaves room for overload, harmonic heating, and eventual dust build up on cooling surfaces. It is often smarter to specify a lower temperature rise than to push the unit closer to its material limits.
Infrared inspection under normal load is the most practical starting point because it reveals loose connections and uneven heating before they become failures. Periodic cleaning of cooling channels and checking enclosure filters matters more than many teams realize. On critical units, continuous temperature sensors embedded in the low voltage windings give early warning of overload or restricted airflow.
Non linear loads create additional winding eddy current losses and can push core temperatures higher than a standard load profile would suggest. The transformer should be derated or designed with a K-factor that matches the actual harmonic spectrum. If the manufacturer cannot provide derating guidance for your load mix, that is usually a sign they are treating the transformer as a commodity rather than an engineered device.
The obvious cases are unusual primary or secondary voltages, tightly constrained footprints, or very high inrush loads that require specific impedance. It also makes sense when the unit feeds a single large drive or furnace where harmonic content and voltage regulation are tightly coupled. A custom unit lets you optimize the winding arrangement and cooling system around the actual duty cycle instead of accepting a compromise that may look fine on paper but struggles in service.
Conclusion
A tour through the winding room often tells you more than any polished datasheet. Tension control, layer insulation placement, and how the coils are handled between stations show whether a builder treats every kVA as a long-term thermal and dielectric system. Material choices matter most at the margins: high-temperature insulation systems, grain-oriented core steel with lower loss density, and conductor cross-sections that avoid hot spots under cyclic loads give industrial units the extra headroom they need when ambient temperatures climb or harmonics push eddy currents higher. The less visible steps can matter even more. Impregnation and cure cycles, if rushed, leave voids that become partial discharge sites or moisture traps. A manufacturer that logs resin viscosity, preheat temperatures, and ramp rates is producing real life expectancy, not just a painted core and coil.
Test reports are where that discipline becomes measurable. Look beyond a pass mark for induced voltage or temperature rise; the actual temperature differentials, insulation resistance values after heat soak, and partial discharge readings indicate whether the builder trusts its own work enough to publish uncomfortable details. Enclosure design then decides how much of that margin survives on site. Vent placement, filter area, bus bar bracing, and air gaps around cable entry points are often overlooked but become the difference between a cool, stable unit and one that derates under heavy industrial load. Before approving a drawing, ask for the assumed ambient and altitude, the short-circuit withstand rating, the expected hot-spot temperature at your real loading profile, and the specific test values on your serial-numbered unit. Builders who answer these directly usually have little to hide.
Contact Us
Contact Person: Kellen Chen
Email: [email protected]
Tel/WhatsApp: 8613806536768
Website: https://www.cnxiaopai.com