Film Sandpaper Manufacturer Reveals Key Considerations for Selecting High Quality Abrasive Films
2026-10-01
When it comes to surface prep and finishing, the difference between a flawless result and a costly rework often comes down to one thing: the abrasive film you choose. But with endless options on the market, how do you separate genuinely high-performing films from those that wear out too fast? That’s where experienced input matters. SHENZHEN SUN ABRASIVES, a film sandpaper manufacturer with hands-on production insight, breaks down the key factors—backing durability, grain consistency, and bond strength—that determine whether an abrasive film can handle real-world demands. If you’re tired of guessing and want to make every sanding pass count, these practical selection tips will give you a clear starting point.
Why Backing Material Is the First Thing to Check
Before you get drawn in by a rug's color or weave, turn it over. The backing is where problems start. A loose, powdery, or brittle backing means the fibers above have nothing stable to hold onto, so the rug will shed, bunch up, and lose its shape within a year or two.
Pay attention to how the backing feels and smells. A strong chemical odor often points to cheap adhesives that will break down quickly, leaving crumbs of latex or glue all over your floor. If you are placing the rug on hardwood or vinyl, avoid thin rubber backings that can trap moisture or react with the floor finish, causing discoloration that is nearly impossible to remove.
How Grit Consistency Shows Up in the Final Surface
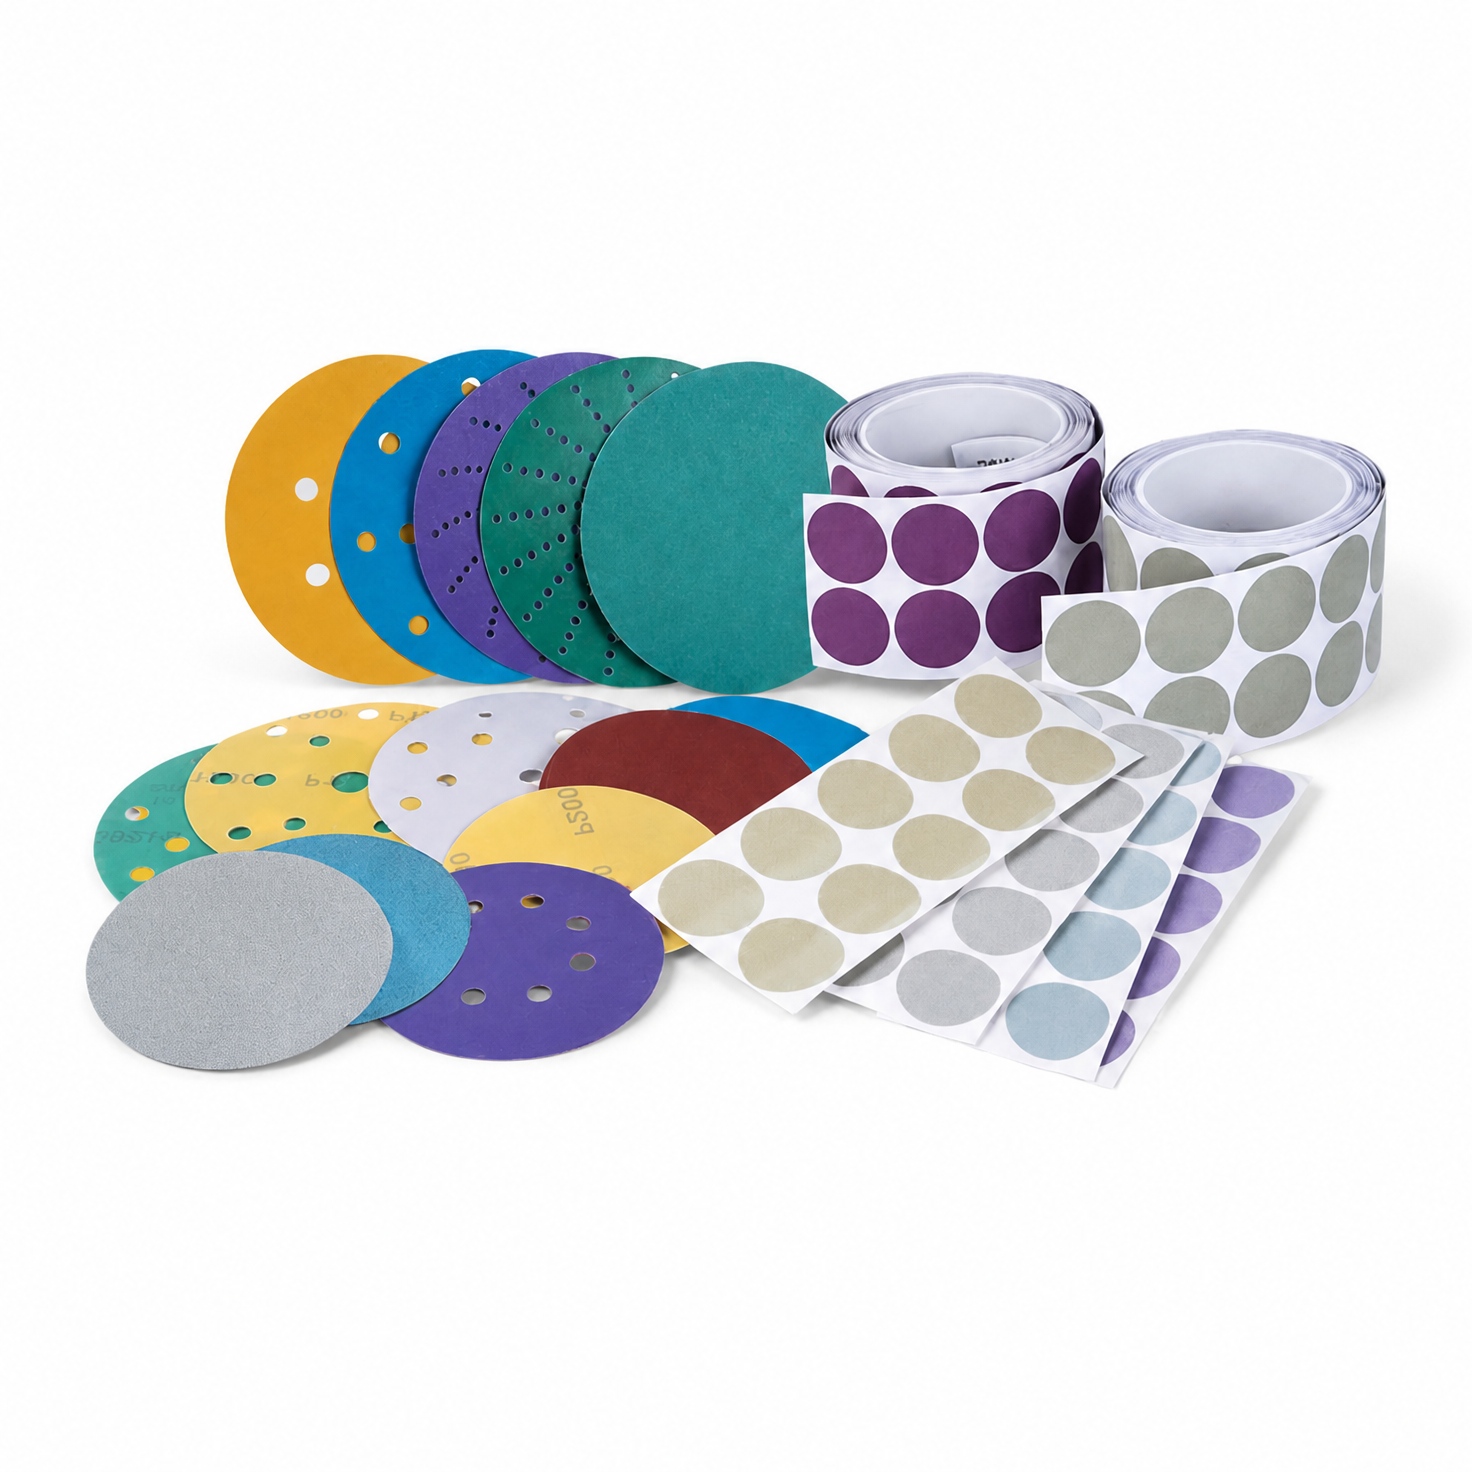
In any abrasive process, the distribution of particle sizes within a grit directly shapes what the eye sees on the finished piece. When that distribution is tight and uniform, the scratch pattern left behind stays even across the entire surface. There's no random deep gouge interrupting the flow, no patch of shallow marks that catches light differently. The result is a predictable, controlled finish that reads as intentional rather than accidental.
Think about a brushed metal panel or a honed stone countertop. If the grit breaks down unevenly or contains oversized particles, the surface picks up a scattered mix of coarse and fine lines. Even after multiple passes, those inconsistencies linger and force the fabricator to overwork the piece just to hide the defects. With consistent grit, each pass removes the same amount of material, so the final texture develops gradually and holds its character from edge to edge.
That reliability matters most when you move from one batch or one tool to another. A tightly controlled grit size means the finish you approved on a sample actually shows up on the production run. It also reduces the need for aggressive rework or extra polishing stages, because the surface doesn't fight back with unpredictable highs and lows. In short, grit consistency is the quiet variable that separates a surface that looks professionally executed from one that looks like it was fought into submission.
The Bond Strength Test Most Buyers Overlook
Most people run a thumbnail across the surface or check how clean the break looks, but that tells you almost nothing about whether a coating or adhesive will stay put six months later. The test that actually matters measures the force required to pull the bonded material away from its substrate, and it is rarely performed before a purchase. Without it, you are gambling on how well the manufacturer controlled cure time, surface prep, and film thickness.
A simple pull-off test using a portable adhesion tester can reveal failures that visual inspection misses. When the dolly pops off, pay attention to where the break occurs. If the adhesive fails at the interface, the bond is weak regardless of how tough the top layer feels. If the substrate itself fractures, that is a different story. Buyers who skip this step often end up blaming the product when the real issue was an untested bond.
The overlooked part is not the machine itself but reading the failure mode. A high number means nothing if the coating peeled away cleanly from the floor. Ask suppliers for this data, or run the test on a small trial area before committing to a full order. It takes an hour and costs less than replacing a failed floor or dealing with a recall later.
Anti-Clogging Coatings Are More Than Just a Buzzword
Plenty of products claim to stop fouling, but the label alone tells you little. A genuine anti-clogging coating works by altering surface energy and roughness at the micron scale, making it harder for proteins, minerals, or biofilms to anchor. In dairy processing, for example, conventional stainless steel lines often need a full hot-water flush every six to eight hours. With a well-matched fluoropolymer or silicone-based coating, the same lines can run for over a day before pressure drop forces a shutdown.
The catch is that “anti-clogging” is not one chemistry. A coating that repels sticky adhesives in a glue dispenser may fail quickly in a wastewater membrane where bacterial slime is the main problem. Inkjet nozzle plates need coatings thin enough not to alter orifice geometry, while medical catheters demand both lubricity and blood compatibility. Matching the coating to the specific foulant, flow rate, and cleaning regime matters more than chasing a generic rating.
Cost is often the reason buyers hesitate, but a narrow focus on price per liter misses the point. Fewer shutdowns mean less downtime and lower cleaning chemical consumption. Over a year, a modest reduction in CIP cycles can offset the initial coating expense several times over. Still, it pays to ask for third-party fouling tests with your actual process fluid, not just a vendor’s glossy comparison chart.
Heat Buildup Is the Silent Killer of Abrasive Film
Most grinding failures aren't dramatic snapshots of a torn belt or a shattered disc. They begin quietly, beneath the surface, as heat accumulates at the grain-workpiece interface. Abrasive film, thin and flexible by design, has nowhere to hide that thermal energy. The resin bond softens, the backing loses its shape, and the cutting edges that once sliced cleanly start to smear and load. You won't hear it or see it right away—just a gradual loss of bite, a need for more pressure, and a finish that goes from satin to scorched without warning.
The real danger is how heat changes the film's behavior long before visible damage appears. As temperatures climb past the resin's glass transition point, the abrasive grains sink instead of stand proud. Instead of cutting, they rub. That rubbing generates more friction, which generates more heat—a loop that quickly turns a precision operation into a polishing smear. Operators often mistake this for dull abrasive and push harder, making things worse. The film may not break, but it stops doing its job, and the workpiece pays the price with thermal discoloration, micro-cracking, or dimensional drift.
Breaking that loop means thinking of heat as a variable you control, not an unavoidable byproduct. Lighter touch, slower feed, intermittent contact, or switching to a film with a cooler-cutting grain like ceramic or a structured abrasive pattern can make a measurable difference. Even something as simple as cleaning the film between passes—removing loaded swarf before it becomes an insulator—buys you time before the heat takes over. The film won't announce its failure. You have to read the signs early, because by the time the surface turns blue, the damage is already done.
Film Thickness and Why One Size Never Fits All
Thickness isn't just a number on a spec sheet; it's the quiet engine behind every performance choice. A film that's too thin might tear under stress or fail to block what it should, while one that's too thick can waste material, add unwanted stiffness, or even create visual distortion. The real skill lies in matching the thickness to the specific job—whether that's a barrier needing only a few microns or a protective layer that must absorb impact without cracking.
Manufacturers often chase a single "ideal" thickness, but that approach ignores how films behave in the wild. Temperature swings, humidity, surface texture, and even the angle of applied force all change what works. A wrap that hugs a curved automotive panel needs a different gauge than a flat window film, even if both claim to be "durable." The sweet spot is always a compromise between protection, flexibility, optical clarity, and cost—and that compromise shifts with every new use case.
What makes this tricky is that thickness doesn't scale in a straight line. Doubling the gauge might triple the puncture resistance but also make the film nearly impossible to apply without bubbles. Conversely, shaving a few microns to save weight can suddenly expose a weak point that wasn't obvious in testing. That's why experienced engineers keep a library of samples—not to find the one perfect film, but to understand how each thickness fails and succeeds under different conditions.
FAQ
Look beyond grit size. The best films use uniformly shaped ceramic or premium aluminum oxide grains that fracture consistently to expose fresh cutting edges, paired with a polyester film backing that resists tearing even when wet. Cheap films often have irregular grain distribution, so they cut unevenly and wear out fast.
Thinner backings—around 3 mil—conform better to contoured surfaces and produce a more consistent scratch pattern on edges. Thicker films, say 5 mil or more, provide extra durability for flat, high-pressure work. Choosing the wrong thickness leads to either premature tearing or poor contact on curves.
Ceramic alumina grains are the top choice for cutting through clear coats and paint because they self-sharpen under heat and pressure. For final finishing, pair them with a fine silicon carbide film, which leaves a shallower scratch profile and reduces the need for heavy compounding.
The resin controls how grains are held and released. A hard phenolic resin keeps grains locked in place for aggressive stock removal, while a softer, more flexible resin lets dull grains shed away, preventing loading and heat buildup. The right balance depends on whether you need fast cut or long life.
Without it, dust clings to the film, clogs the abrasive, and forces you to change sheets more often. A well-applied anti-static coating lets dust fall away or extract cleanly, which keeps the cutting surface open and dramatically extends the working life of each sheet.
Yes, to a point. A quality film has a consistent, slightly stiff feel with no thin spots or bubbles when you run your fingers across the surface. Bend it—if the backing cracks or the grains flake off at the crease, it won't survive tight contours or repeated flexing during hand sanding.
Don't jump more than 50% in grit number between steps. For example, go from 320 to 400 to 600, not 320 straight to 800. Each finer film should remove the previous scratches completely. Rushing the sequence leaves deep scratches that show up only after clear coat is applied.
Conclusion
A film sandpaper manufacturer walks through what actually separates reliable abrasive film from the rolls that fail early. The backing is not just a carrier; it dictates tear resistance, flexibility, and how evenly pressure transfers to the grain. If the backing stretches or breaks down under heat, even premium abrasive grain will underperform. Grit consistency shows up in the final surface—if grain sizes vary, scratches won't be uniform, and rework becomes unavoidable. A tight size distribution is what lets fine finishing feel predictable. Most buyers overlook the bond strength test, but a simple flex or rub test reveals whether the resin can hold the grain through the intended pass count. Weak bonding means more grain shed and shorter life, no matter how sharp the mineral is.
Anti-clogging coatings earn their keep when sanding paints, primers, or soft metals; they prevent swarf from packing the surface and help each sheet cut longer. These coatings are not just a marketing term—they reduce the need to clean or replace film mid-job. Heat buildup is the silent killer because excess temperature softens the resin and shortens abrasive life, so films that dissipate heat tend to outlast thicker but hotter-running alternatives. Film thickness varies by application: thin films conform to contours and reach into profiles, while thicker films give the stiffness needed for flat, aggressive stock removal. One size never fits all, and a manufacturer that asks about your substrate, finish expectations, and machine speed is usually the one whose film will hold up in real use.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn