Tissue Converting Equipment Manufacturer Reveals Proven Strategies for Higher Output
2026-09-19
What if the bottleneck in your tissue converting line isn’t the equipment itself, but the way it’s been configured—or the small inefficiencies that quietly pile up shift after shift? As a tissue converting equipment manufacturer that works with converters every day, DAXIN has seen firsthand which changes actually move the needle on output. The strategies below aren’t recycled theory; they come from real production floors where line speed, waste, and downtime were rebalanced to squeeze out more capacity without a full capital investment. If your current numbers feel stuck, one of these proven levers might be the missing piece.
Where Tissue Lines Lose Speed Without Anyone Noticing
In tissue converting, most slowdowns never show up on a downtime report because they happen inside normal run cycles. A splicing unit that hesitates a half-second longer, a tension dancer drifting out of its sweet spot, or a slight reduction in unwind speed to compensate for a wobbling parent roll all chip away at line speed without tripping an alarm. These micro-delays are rarely logged.
The problem compounds in older machines where PLC setpoints get nudged downward operator by operator. One shift lowers the max draw to prevent edge wrinkling; another trims the embosser speed to quiet a bearing. Each change is rational on its own, but after a year the line's true capability is buried under dozens of small, forgotten compromises. No one notices because the line still produces, just slower.
Even energy management systems can mask losses. A dryer hood that responds to moisture swings by backing off the burner also forces the reel to ease up, and that reduction becomes the new baseline. By the time anyone compares current output to the original design spec, the tissue line has lost several percentage points of throughput — silently accepted as "how the machine runs now."
Why Standard Tension Settings Rarely Fit Real Production Runs
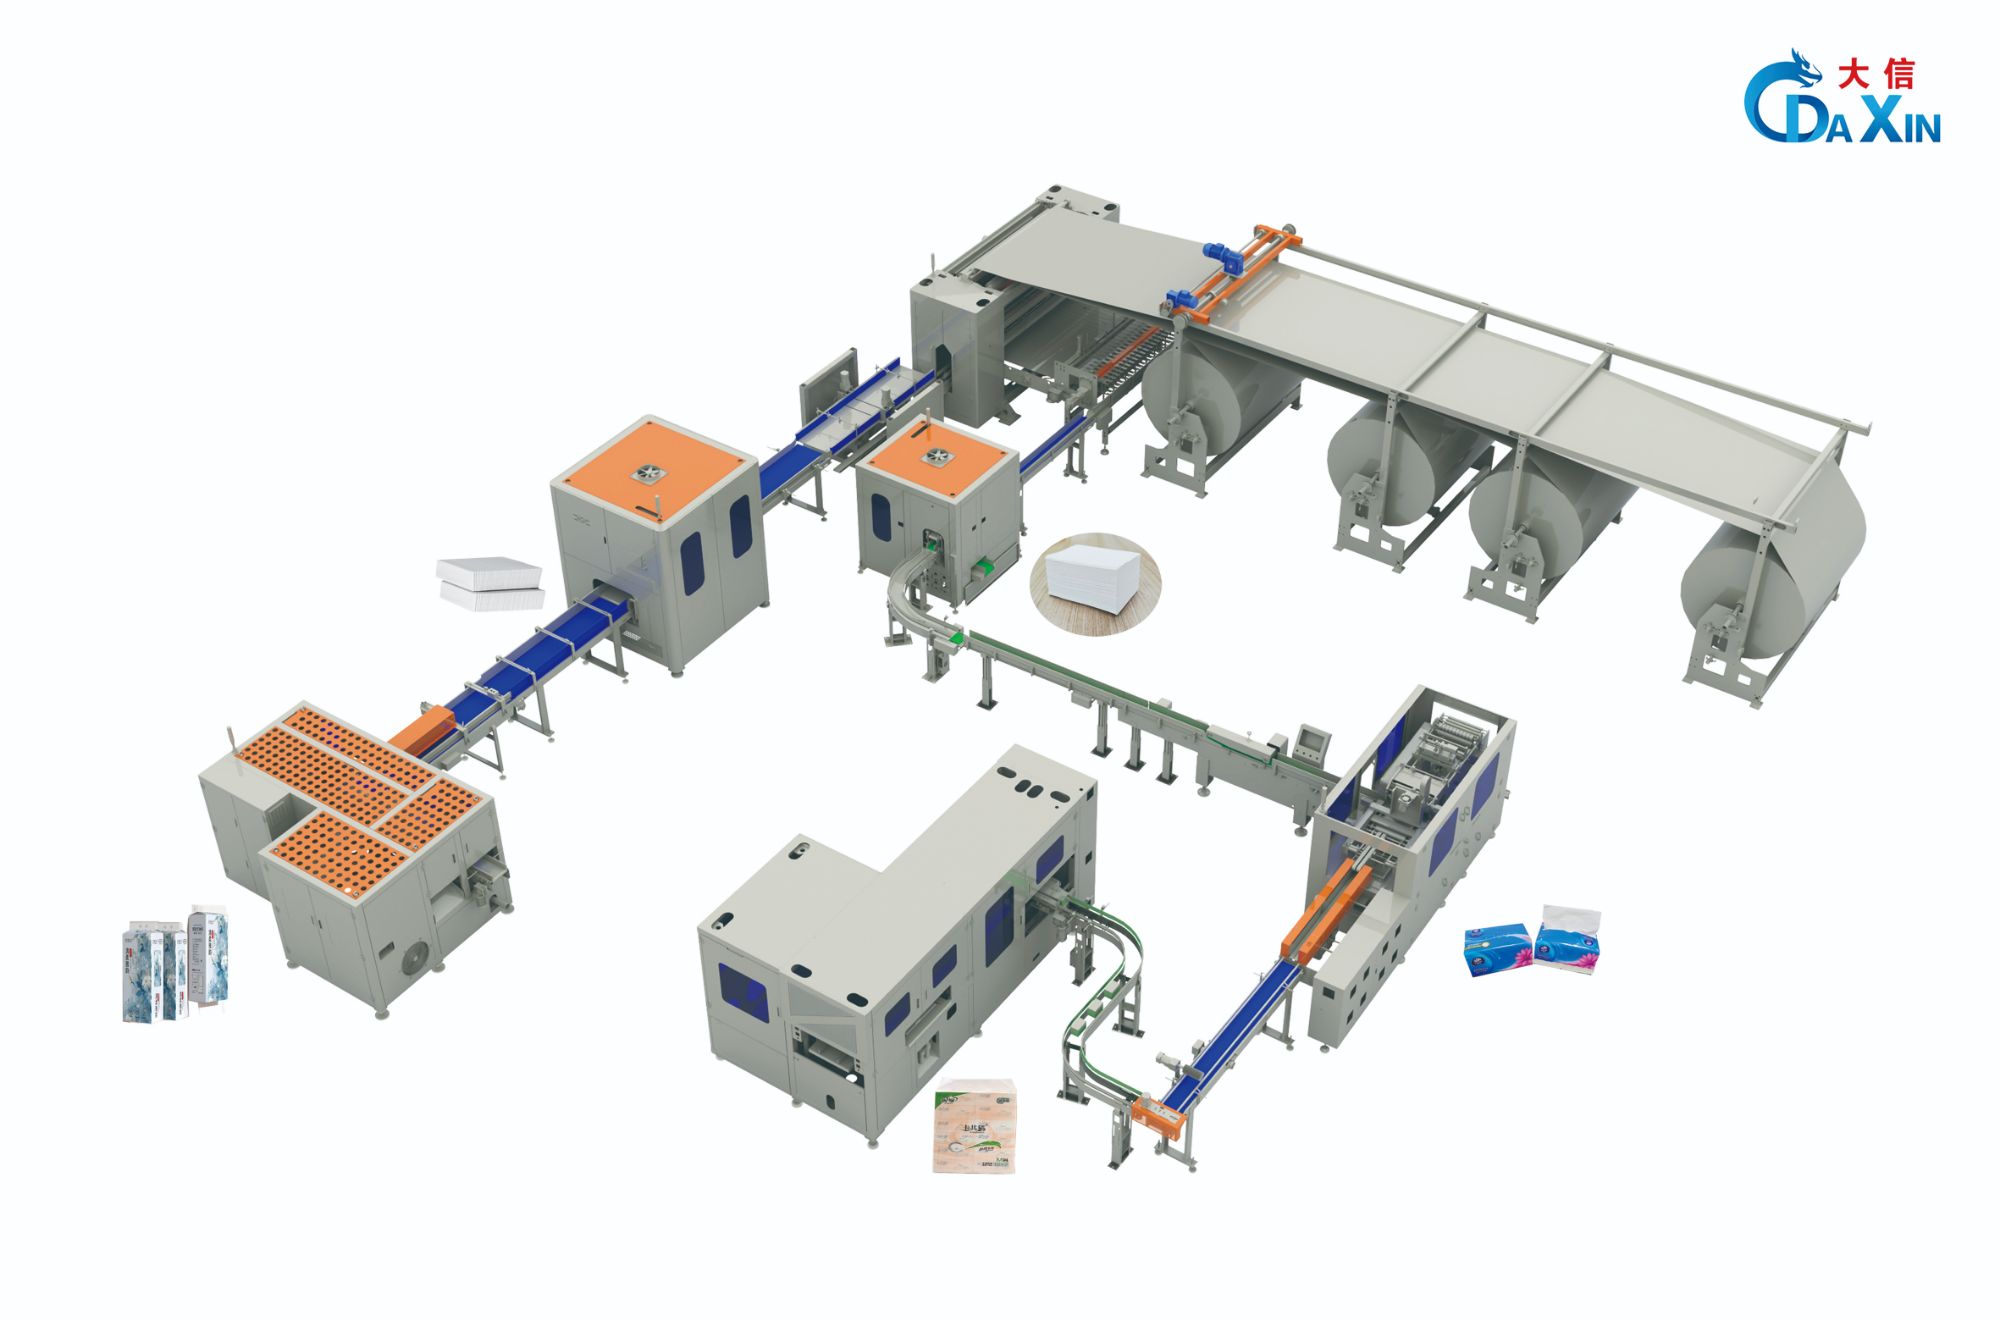
Walk onto any production floor and you'll hear the same story: the spec sheet says one tension, but the machine runs better at another. Standard tension settings are derived from controlled lab conditions—clean threads, consistent material thickness, ideal temperature. Real runs rarely behave that way. Bobbins heat up, fabric relaxes, needle plates wear, and suddenly the recommended number is just a starting point, not a finish line.
What makes it worse is that operators learn to distrust the manual. They see skipped stitches at the prescribed setting, then nudge the dial until the seam looks right. That nudge becomes tribal knowledge, passed from shift to shift but never written down. The result: every line develops its own "correct" tension, measured by feel and sound more than by any gauge.
The fix isn't tighter specs or fancier meters. It's accepting that tension is a living variable. Build in a tuning window, document the actual settings per machine and material combo, and stop pretending one number fits all. The best shops I've visited treat tension like seasoning—adjust, taste, repeat. The worst treat it like a law that only works in the lab.
The Case for Slowing Down to Speed Up Changeovers
Most changeover improvement efforts start with a stopwatch and a sense of urgency. The instinct is to move faster: grab tools sooner, rush the adjustments, skip the coffee break. Yet that hurry often hides the real cost. When a setup is treated as a race, small mistakes compound—a misaligned fixture here, a missing torque spec there—and the line ends up stopping again minutes later. Slowing down just enough to watch the entire sequence with fresh eyes reveals where the actual time goes.
A slower, deliberate pass through a changeover lets you separate what must happen while the machine is down from what could have been done beforehand. Often the biggest wins come from simple observations: a gauge stored three steps too far away, a bolt that needs replacing because the threads are worn, a checklist that skips a critical verification. These discoveries rarely surface when people are sprinting. By walking through each motion without the pressure to beat the clock, the team can eliminate wasted movement, pre-stage materials, and convert internal tasks into external ones.
The irony is that this temporary slowdown produces a faster, more repeatable changeover in the long run. Once the new sequence is practiced and standardized, the crew moves with quiet confidence instead of frantic energy. Downtime drops not because individuals work harder, but because the process no longer fights itself. Slowing down to understand the work is not a delay—it is the fastest route to a setup that actually sticks.
How Blade Wear Data Predicts Output Drops Before They Happen
Blade wear rarely announces itself with a sudden snap. Instead, it leaves a trail of subtle performance shifts that, when read correctly, tell you exactly when output will start to slide. Vibration signatures change first—tiny increases in high-frequency harmonics that standard monitoring often dismisses as noise. By tracking these small deviations against historical baselines, you can spot the early stages of edge rounding long before visible damage appears. The data acts like a weather forecast: not a guarantee, but a probability curve that sharpens with every new data point.
The real predictive power comes from correlating wear metrics with actual throughput. A blade that has lost only 3% of its cutting edge may already be consuming 7% more energy per unit, while scrap rates tick upward by fractions of a percent. These relationships are rarely linear, which is why simplistic threshold alarms fail. Building a rolling model that ties wear indicators to output efficiency lets you project the exact day when the drop becomes unacceptable—and schedule maintenance during planned downtime instead of reacting to an emergency stop.
What separates useful predictions from noise is context. Ambient temperature, material batch variations, and even operator habits can mask or mimic wear signals. The trick is to feed all of that into the same model, letting the algorithm learn which combinations actually precede output drops. Over time, the system begins to recognize patterns that no single sensor could reveal—like the fact that a certain vibration frequency combined with a slight motor current rise on Tuesday shifts means a 90% chance of a 5% output loss by Friday. That's not magic; it's just paying attention to the right data in the right way.
Rethinking Operator Training for Small, Frequent Adjustments
Most operator training still treats production as a steady state. It walks people through a fixed sequence of steps and assumes the line will behave the same way tomorrow. But in many plants, the real work is a series of small, frequent adjustments—tweaking a feed rate here, nudging a temperature setpoint there. When training ignores this reality, operators leave the classroom knowing the ideal procedure but not how to respond when the process drifts slightly out of spec. That gap shows up quickly on the floor as hesitation, overcorrection, or someone waiting for a supervisor instead of acting.
A better approach flips the focus from memorizing steps to reading signals. Short, scenario-based drills work well: give an operator a barely-off trend line, a subtle pressure change, or an unusual sound from a pump, and ask what they would check first. The goal isn’t to rehearse a perfect answer but to build a feel for when a small adjustment is needed and which direction makes sense. Pairing new hires with experienced operators for a few weeks of real-time shadowing also helps, as long as the veteran explains the “why” behind each tweak rather than just making it.
Measuring the success of this training also has to change. Instead of tracking module completion or test scores, look at how quickly operators spot a developing issue and whether their first adjustment brings the process closer to target or makes it worse. A simple log of small adjustments—what was changed, why, and the result—can reveal patterns and turn everyday corrections into a shared learning tool. Over time, this builds a team that is comfortable with constant minor variation instead of being paralyzed by it.
What High-Mix Orders Do to Idle Time (and How to Reverse It)
The moment a production line shifts from a familiar part number to a low-volume variant, the clock starts working against you. Operators wait for new tooling, machines sit cold during program swaps, and supervisors chase missing setup instructions. These small gaps multiply quickly; a two-minute pause might not look serious on paper, but across forty changeovers a day it becomes hours of lost capacity. High-mix work doesn't just add direct setup time—it exposes every weak point in your scheduling, material staging, and shop floor communication.
Much of that idle time hides inside the gaps between 'last good piece' and 'first good piece.' Forcing teams to perform changeovers in a fixed sequence, or requiring a single skilled technician to handle every adjustment, turns a routine transition into a bottleneck. The fix usually isn't buying faster machines. It's shrinking the distance tools travel, pre-kitting the next job while the current one runs, and giving operators the authority to make standard adjustments without waiting for approval. When the next order's fixtures, programs, and materials are already at the machine before the last part leaves it, the line doesn't feel the mix.
Reversing the trend starts with tracking where the minutes actually go. A simple log of changeover start and stop times often reveals that most idle time comes from three or four stubborn steps: searching for tools, reprogramming offsets, or clearing leftover material. Tackle those few steps first, even with low-cost fixes like shadow boards and staged carts, and the gains stack up fast. Over time, grouping similar geometries or materials in the schedule further reduces the frequency of major swaps. High-mix will never behave like dedicated mass production, but it doesn't have to leak hours every day.
FAQ
Look at the unwind and splicing cycle before adjusting line speed, because a poorly timed splice or wrinkled parent roll often costs more runtime than a modest speed increase.
Higher speeds amplify small misalignments in embossing or perforating units, so waste rises unless roll balancing and blade registration are tightened first.
They focus on reducing micro-stops around log saws and tail sealers, standardize roll diameters, and adjust tension profiles to allow faster ramp-ups after splices.
Operators who can diagnose the difference between a dull blade and a tension drift tend to react faster and avoid repeated trial-and-error stops, which keeps lines running longer.
Daily checks of perforation blade sharpness, embosser roll alignment, and adhesive application nozzles prevent most of the small stops that quietly erode daily output.
Run a shift at the higher speed and measure net good rolls produced per hour, not just line speed, because waste, jams, and rework can cancel the apparent gain.
Conclusion
Many tissue converting lines lose speed gradually without operators noticing—small slowdowns from worn belts, misaligned rollers, or drifting tension settings accumulate into serious output losses. Standard tension presets rarely match real production runs because basis weight, humidity, and roll hardness vary shift to shift. A proven approach is to have operators record actual tension values at start-up and after each splice, then adjust to a narrow band based on observed web behavior rather than factory defaults. Similarly, deliberately slowing down during changeovers—running the line at half speed while verifying knife positions and core seating—often cuts total downtime more than rushing through setup. Slowing the ramp-up phase by just a few seconds prevents miswraps and torn tails that would otherwise force a full restart.
Beyond mechanical tweaks, manufacturers can use blade wear data to predict output drops before they happen. By logging cuts per blade and tracking edge quality, converters spot a dull blade trend days ahead of a jam or ragged perforation. Pairing that with operator training focused on small, frequent adjustments—rather than waiting for major faults—keeps the line in a tighter operating band. High-mix order patterns also create hidden idle time through repeated wash-ups and splice changes. Reversing that means grouping similar substrates, pre-staging cores and knives for the next job, and making changeover tasks visual so crews can move without waiting for instructions. These practical strategies, taken together, raise throughput without adding capital equipment.
Contact Us
Contact Person: Sam Xie
Email: [email protected]
Tel/WhatsApp: 86-18938538530
Website: https://www.daxin321.com/