Top 10 Pet Food Production Line Solutions for Growing Manufacturers
2026-10-10
Pet food manufacturing is unforgiving to outdated lines. One slow mixer or inconsistent extruder can throttle an entire operation. We looked at what actually moves growing brands forward—throughput, flexibility, and uptime—then narrowed the field to ten standout production line solutions. From compact systems to full-scale plants, each entry earns its place by solving a specific growth challenge. And yes, MINGDE makes the cut for reasons you'll want to read about.
Modular Extrusion Lines That Start Lean and Add Capacity in Place
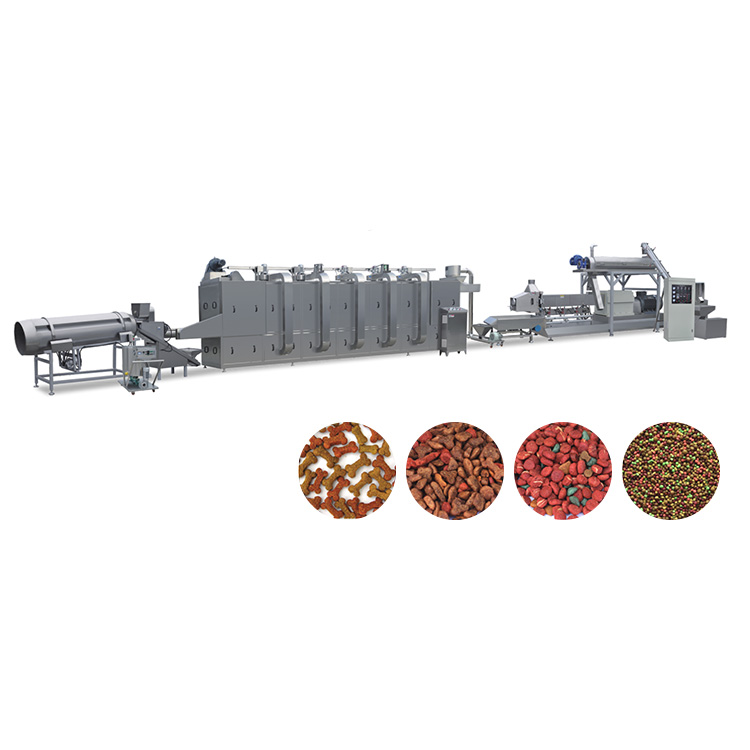
A modular extrusion line can begin with just the core elements—extruder, die, and a basic cooling tank. That compact footprint keeps initial investment lean and lets a processor start running profiles without paying for capacity that may never be needed. When orders grow, additional modules such as vacuum calibration, extra cooling baths, a belt haul-off, or an in-line cutter slide onto the same frame. There is no need to tear down walls or pour new foundations.
Because each module carries its own drives, sensors, and quick-connect utilities, expansion happens during a scheduled downtime window rather than a full plant shutdown. A processor can add a second haul-off for thin-wall profiles or swap calibration tooling for a different shape, then resume production with the same operator interface. That in-place growth makes the line adapt to product mix changes without losing the floor layout you already know.
Gentle Ingredient Conveying for High-Meat and Freeze-Dried Recipes
High-meat and freeze-dried recipes demand a handling method that respects the raw ingredients from start to finish. Instead of harsh extrusion or prolonged high-heat cooking, the process relies on low-temperature moisture removal that keeps muscle fibers and organ meats intact. This gentle approach preserves the natural aroma, texture, and nutrient density that pets notice at first sniff.
The ingredient stream stays minimal on purpose. Whole cuts, finely ground bone, and nutrient-rich organs move through a cold blending stage before freeze-drying, so fats and amino acids are not exposed to damaging temperatures. Because the recipe includes very little carbohydrate or filler, the physical conveying system must avoid crushing delicate morsels or causing oil separation. Slow, short-distance transfers and clean, cooled contact surfaces do that work quietly.
The result is a dry food that rehydrates into something close to a raw meal’s softness and smell. Picky eaters often respond to the unchanged protein scent, while sensitive stomachs benefit from a formula that has not been repeatedly cooked. In a high-meat context, gentle ingredient conveying is not just a production detail; it shapes how the finished recipe behaves in the bowl.
Recipe Memory Systems That Cut Setup Time Between Trial Batches
When a bench chemist finishes one trial batch and starts another, the clock starts ticking. Most of the delay isn't the actual mixing or heating—it's the hunt for the last run's settings. Scribbled notes, outdated spreadsheets, and half-remembered valve positions all eat into the window for real experimentation. A recipe memory system fixes that by treating every batch like a saved file. One tap pulls up the full parameter set: ingredient weights to the gram, ramp rates, hold times, and even which pump was used. No retyping, no guessing.
The real payoff comes from how these systems structure the handoff. Instead of just storing numbers, they group settings by trial ID and version. When a formulation changes mid-study, the system logs the delta—only the altered steps are highlighted for review. That means an operator can switch from a high-shear granulation to a low-viscosity coating run in under ten minutes. The equipment still has to be physically cleaned and reconfigured, but the software pushes the new setpoints to the PLCs before the operator finishes the washdown. Downtime drops because the thinking part is already done.
One dairy pilot facility cut its changeover time from 42 minutes to 11 after adopting recipe memory across five mixing vessels. The system also flags mismatched parameters—like a pasteurization temperature that doesn't match the current product spec—so a wrong batch never gets started. Because the cleaning cycles are tied to each recipe, cross-contamination risks drop too. The result is more trial batches per shift and fewer scrapped runs, which is exactly what an R&D team needs when every hour counts.
Coating and Toasting Steps Tuned for Small-Batch Flavor Launches
When you're rolling out a limited run, every gram of coating and every second in the toaster matters more than it ever does at scale. We start by holding back a portion of the seasoning blend to dust on mid-toast, which builds a layered crust instead of a one-note shell. For small batches, a gentle tumble in a wide, shallow pan keeps the coating even without crushing delicate edges—something a big industrial drum just can't replicate.
Toasting gets dialed in by feel rather than fixed timers. Lower heat with a few extra flips lets the sugars in the coating caramelize slowly, giving each piece a deeper color and a crunch that snaps instead of shattering. We'll often pull a test piece at the halfway mark, break it open, and adjust the next round's moisture or oil level on the spot. That kind of on-the-fly tuning only works when you're working with a few kilos, not a few hundred.
For flavor launches, we lean into small-batch quirks: uneven toasting isn't a flaw, it's a signature. A slightly darker edge here, a lighter patch there—it tells the taster this wasn't made on an assembly line. Keep the coating rustic, let the toast carry a whisper of smokiness from a hot spot, and document every tweak in a simple log so you can repeat the happy accidents on the next limited drop.
Drying and Cooling Zones That Keep Kibble Texture Consistent
In a continuous extrusion line, the drying zone is rarely a single-temperature chamber. Instead, it's split into staged sections where warm air passes through the product bed at different velocities and humidity levels. This staged approach lets moisture leave the kibble from the inside out, preventing the outer shell from sealing too early—a common cause of uneven crunch. Operators typically monitor the exhaust air moisture rather than just inlet temperatures, because that tells you when the surface is releasing water faster than the core can supply it.
Cooling is just as critical, but it's often treated as an afterthought. A kibble that exits the dryer at 70–80°C still holds residual heat that can continue cooking the starch matrix if not removed quickly. Counter-flow coolers with ambient or chilled air lower the core temperature without shocking the structure. The trick is to avoid a sharp temperature drop across the exterior, which creates micro-cracks that only show up later as broken pieces at the bottom of the bag. Gentle, progressive cooling keeps the cell walls intact.
What makes the drying and cooling zones work as a system is the handoff between them. If the drying curve ends too wet, the cooler has to compensate by pulling more moisture, but that often leaves the kibble with a dry, brittle crust over a soft center. Conversely, over-drying before cooling wastes energy and can lead to excessive fines during packaging. By synchronizing the residence time in both zones—and using in-line moisture sensors at the boundary—the texture remains consistent batch after batch, with a uniform snap and density that pet owners notice when they pour a fresh bowl.
Case Packing and Palletizing Designed for Mixed SKU Runs
Mixed SKU runs used to force a choice between throughput and flexibility. New case packing and palletizing equipment removes that trade-off. The system reads each carton as it enters the cell—checking dimensions, weight, and destination—then builds the pallet layer by layer without relying on preset patterns. Operators can feed random sequences of products and still get stable, shippable loads at full line speed.
The shift comes from software that treats every case as a unique item rather than part of a homogeneous batch. Layer planning happens continuously, so a tall narrow carton and a flat wide one end up where they support the load best. When the product mix changes from one hour to the next, there is no mechanical adjustment or pause for reprogramming. The palletizer simply recalculates the next best position and keeps moving.
This approach changes how warehouses think about late-stage customization. Mixed SKU pallets can be built directly for store-ready delivery or regional distribution without manual sorting upstream. The combination of adaptive grippers and real-time layout logic means each pallet arrives dense, balanced, and ready for the next leg of the supply chain.
FAQ
Look closely at how easily the system can scale without forcing a full redesign. Modular stations for mixing, extrusion, drying, and coating let you add capacity in stages, while quick-change die plates and adjustable cutter speeds reduce downtime between product runs. Also check whether control systems allow recipe storage and automatic parameter tracking, because that saves operators from manual guesswork as volumes increase.
Extrusion is where texture, density, and nutritional consistency are largely decided. Modern lines with precise barrel temperature zones and variable screw speeds can handle high-meat inclusions, sensitive ingredients, and shapes ranging from kibble to semi-moist treats. Better control over shear and residence time means fewer rejected batches and more freedom to launch differentiated formulas without buying separate equipment.
Sanitary design matters more than many realize. Look for sloped surfaces, minimal crevices, tool-free access to critical areas, and stainless steel contact parts. Integrated metal detection and in-line moisture or temperature sensors give continuous verification, while automated cleaning cycles and easy-to-remove die assemblies reduce contamination risk between allergen or recipe changes.
Automation shifts the bottleneck from manual supervision to system-level monitoring. Centralized PLC or SCADA interfaces let a small team manage batching, extrusion parameters, drying profiles, and packaging feeds from one screen. Automatic adjustments based on real-time moisture data or product density feedback cut operator intervention, so you can run longer shifts with fewer skilled workers and still maintain uniform output.
Choose equipment that supports rapid changeovers and a broad recipe window. If the line can switch between dry kibble, semi-moist, and high-protein treats without major mechanical modifications, you can respond to niche demands faster. Also favor suppliers that offer software updates, additional coating drums, or vacuum infusion modules as add-ons, because retrofitting is usually cheaper than replacing the whole line.
Many buyers overfocus on initial throughput and ignore changeover time, utility consumption, or spare parts availability. A line that runs at high speed but takes hours to clean between recipes can hurt more than help. Another mistake is underestimating the importance of local service support and training, because downtime from a failed sensor or misaligned cutter can erase the savings from a lower upfront price.
Drying locks in shelf stability and microbial safety, while coating applies fats, palatants, and functional ingredients that drive acceptance. A poorly controlled dryer can cause case hardening or uneven moisture, leading to mold risk and texture complaints. Coating systems with precise spray nozzles and gentle mixing preserve the kibble shape and ensure consistent flavor distribution, which directly affects repeat purchases.
Conclusion
For growing pet food manufacturers, the leap from pilot batches to full-scale production often exposes hidden bottlenecks. Modular extrusion lines solve this by allowing you to start lean with a single screw configuration, then add preconditioning barrels or die faces in place as demand climbs. Paired with gentle ingredient conveying tailored for high-meat and freeze-dried recipes, these systems preserve protein integrity and prevent smearing, which is critical when raw inclusions exceed 60%. Recipe memory systems further compress setup time between trial batches, letting operators recall exact barrel temperatures, screw speeds, and steam injection profiles from a touchscreen instead of re-tuning from scratch. This combination means a small team can run multiple niche formulations in a single shift without sacrificing consistency.
Where flavor and texture become competitive edges, small-batch coating and toasting steps make all the difference. Tuned tumblers and infrared toasting zones allow you to launch limited-edition kibble toppers or freeze-dried raw blends without committing to a full production run. Downstream, drying and cooling zones with segmented airflow control keep kibble texture consistent across batches, eliminating the dreaded brittle center or soft shell. Finally, case packing and palletizing designed for mixed SKU runs use vision-guided picking and on-the-fly label verification to handle multiple bag sizes and retail-ready trays without manual changeovers. Together, these six strategies form a cohesive road map: invest in flexible, memory-driven upstream equipment, then match it with agile finishing and packing lines—so growth never forces you to choose between speed and artisanal quality.
Contact Us
Contact Person: LILY SUN
Email: [email protected]
Tel/WhatsApp: 0086-13969103791
Website: https://www.snackfoodmachinery.com/